Packaging blog
Custom Retail Packaging Design Checklist
The structural, regulatory and production checks worth completing before packaging artwork goes to press, ordered the way production actually needs them.
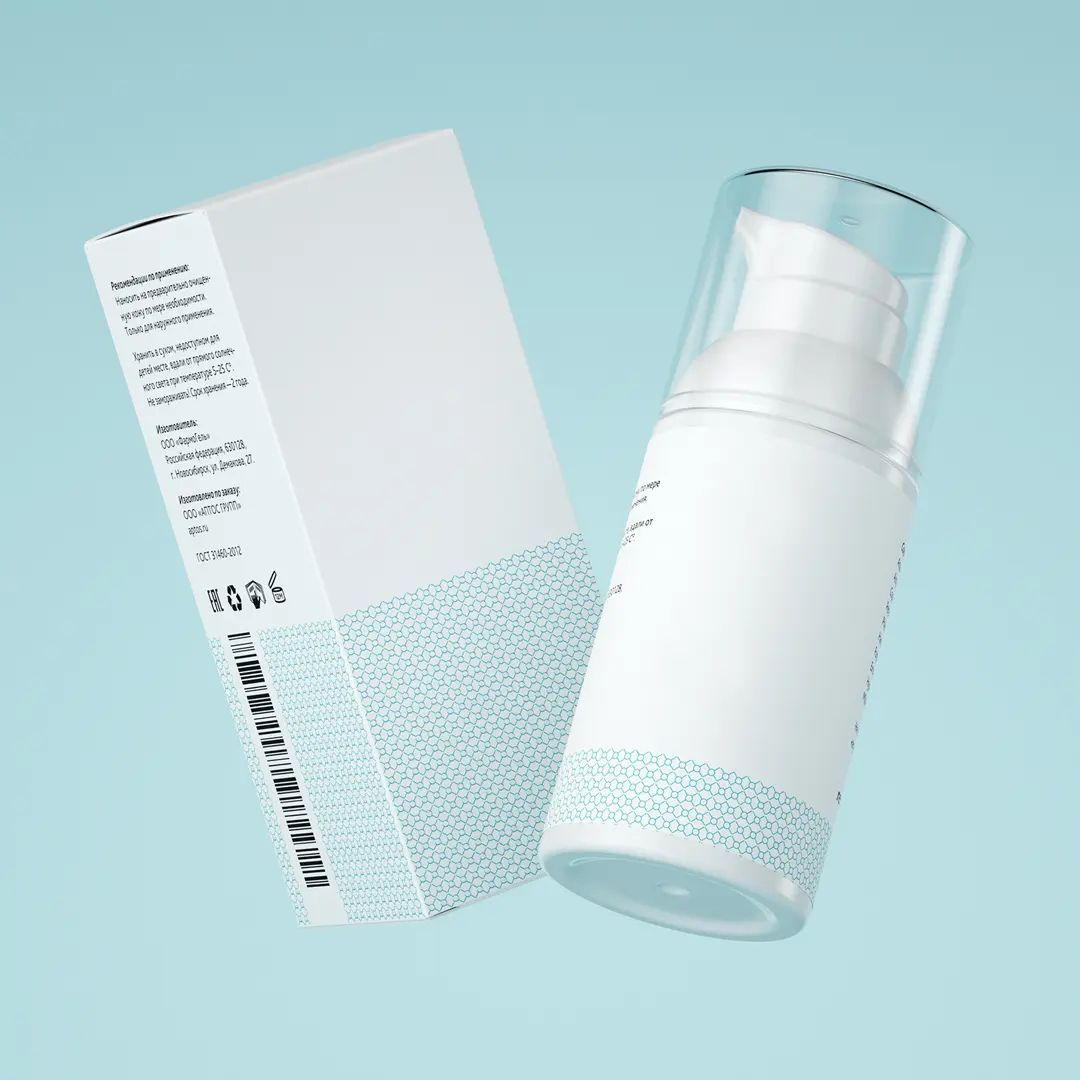
Packaging artwork gets rejected at prepress for the same handful of reasons, year after year. Almost none of them are design failures. They are process failures — a step skipped, a measurement taken from the wrong place, a panel laid out before anyone checked what legally had to fit on it.
This checklist follows the order production actually needs, which is not the order most people work in.
Confirm the structure before opening a design file
Nothing in artwork can be finalised until the dieline exists, because the dieline defines where every panel edge, fold and glue tab sits.
Check that the product has been measured at its widest point in all three dimensions, and measured in the state it will be packed in. Confirm the weight, because that determines board grade, and board grade slightly changes the internal dimensions of a folded carton.
Confirm whether an insert is needed. Adding one later changes the outer dimensions, which changes the dieline, which invalidates the artwork.
Work on the supplied dieline, not a rectangle
Design directly on the dieline template your supplier provides. Import it as a locked layer and keep it locked.
The dieline carries information a plain rectangle does not: fold lines, glue tabs, tuck flaps, the direction each panel faces when assembled, and which areas are hidden after gluing. Artwork built on a guessed rectangle almost always places something important across a crease or under a glue lap.
Keep the dieline layer out of the printed output. It should be visible for positioning and excluded from the exported print file, usually by setting it to a non-printing spot colour.
Set up bleed, safety and trim correctly
Three checks here, and all three fail regularly.
Bleed extends artwork past the trim edge so that a small cutting variance does not leave a white sliver. For folding cartons, 3 mm past every trim edge is standard. For rigid box wraps it is far larger — typically 15 mm — because the paper turns in around the board.
Safety margin holds critical content away from the edge. Text and logos should sit at least 4 mm inside any trim or fold line. Anything closer risks being cut through or folded across.
Check that fold lines do not run through type. A headline crossing a crease looks like a production error even when it was intentional.
Lay out the regulated panel first
This is the step most often left until last, and it is the one most likely to force a redesign.
Work out exactly what the law requires on your pack before you position anything decorative. Food needs an ingredient list, allergens and net weight. Cosmetics need an INCI panel. Supplements need a supplement facts panel in a prescribed layout. CBD products need state-specific warnings, and those vary by where the product is sold. California sales may require a Proposition 65 warning.
Set that content at its real, final length and at the minimum legible size, then design around what remains. Designing first and squeezing the panel in afterwards produces packs where the ingredient text is unreadably small, which is both a compliance risk and a bad customer experience.
Check colour is defined the way it will print
Convert everything to CMYK unless you are printing spot colours, in which case define those as named spot swatches rather than CMYK approximations.
Rich blacks need a build, not 100% K alone, which prints as a washed grey on large areas. A common build is 60C 40M 40Y 100K, though your printer may specify their own. Small text should stay 100% K only, because a four-colour build on small type shows registration fringing.
Be realistic about colour on uncoated stock. If you are printing on kraft or uncoated board, colours will appear duller and warmer than they do on screen or on a coated proof. Ask for a proof on the actual substrate if colour accuracy matters.
Verify image resolution and linked assets
Every raster image should be 300 dpi at its final placed size, not at its original size. A 300 dpi image scaled up 200% is effectively 150 dpi and will look soft in print.
Check that all links are present and embedded before export. Missing links are one of the most common reasons a file bounces back from prepress.
Vector artwork should stay vector. Logos rasterised at some point in their history and reused ever since are a recurring source of soft edges on printed packaging.
Confirm barcodes will actually scan
Barcodes fail more often than people expect, usually for three reasons.
The barcode is placed across a fold or a curved surface, so the scanner cannot read it in one plane. It is scaled below the minimum size for its symbology. Or it is printed in a colour combination with insufficient contrast — red on white does not scan reliably, and light bars on a dark background do not scan at all without inversion support.
Place barcodes on a flat panel, keep them at or above 80% of nominal size, and print them dark on light with a clear quiet zone around them.
Run the pre-press checks yourself
Before sending, work through these:
- Fonts outlined or fully embedded
- All images 300 dpi at placed size and CMYK
- Bleed applied on every trim edge
- Critical content inside the safety margin
- Dieline on a separate non-printing layer
- Spot colours named consistently, no stray unused swatches
- Overprint settings checked, especially on white objects
- File exported as a print-ready PDF with the correct preset
- Total ink coverage within the printer’s limit, usually around 300%
Approve a proof against the real thing
A digital proof confirms content and layout. It does not reliably confirm colour, because your screen and the press are different devices.
If colour is critical, ask for a hard proof on the actual substrate. If structure is critical, ask for a plain unprinted sample and put the real product inside it. Do both if the run is large enough to justify it — the cost of a sample is trivial against the cost of reprinting several thousand units.
Check the proof against a printed list of what you asked for, not against your memory of it. Approvals given from memory are how the wrong version of a panel reaches production.
Keep the files for reorders
Once a run completes, archive the approved print file, the dieline, the board specification, the finish list and the colour targets together.
Reorders are far cheaper and faster when nothing has to be rebuilt, and consistency between batches is one of the things retail buyers notice. Suppliers should hold this on file as well, but a brand that keeps its own copy is never dependent on that.
For a fuller technical breakdown of file setup, our dieline and artwork preparation guide covers export settings and template handling in more detail.