Packaging resources
Box Style Guide
Folding cartons, mailers, rigid boxes, display units and trays compared on construction, assembly, shipping and where each style stops working.
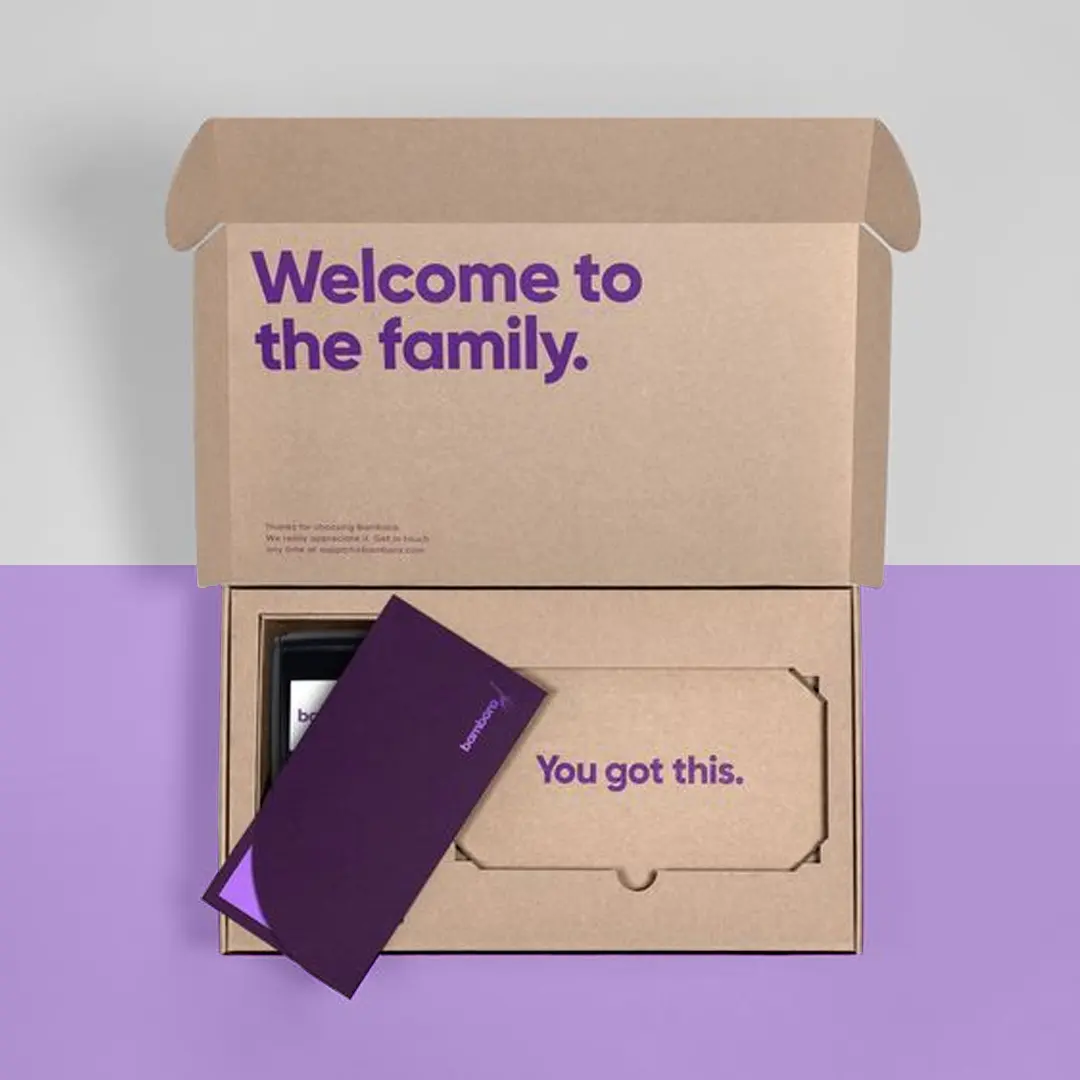
Box style is a structural decision made before material, size or print. Each style is manufactured differently, ships differently and has a natural range beyond which it stops making sense.
Straight tuck end and reverse tuck end
The most common folding carton styles. Both are die-cut from one sheet, glued along a single seam, and ship flat.
Straight tuck end has both flaps folding in the same direction, which gives a cleaner front face. Reverse tuck end alternates them, which uses slightly less board and costs marginally less.
Best for light retail products up to about three pounds. Both are inexpensive and fast to produce.
Snap-lock bottom and auto-lock bottom
Where a tuck-end carton would not hold the weight, a locking base does. Snap-lock bottoms are assembled by folding tabs into place. Auto-lock bottoms spring open when squeezed, which is much faster on a packing line.
Auto-lock costs more per unit but pays back in labour where volumes are high.
Roll-end tuck front (mailer box)
The e-commerce standard. Cut from single-face corrugated with integrated side wings and a front tuck, it assembles without tape and survives carrier handling.
Ships flat and score-folded, assembles in seconds by hand, and the interior face is visible at opening — which is why interior printing matters on this style.
Regular slotted container
The classic shipping box, with flaps meeting at the centre on top and bottom. Cheapest corrugated construction per unit because it wastes almost no board. Requires tape to close, so it is a shipper rather than a presentation pack.
Rigid two-piece and hinged lid
Base and lid built separately from wrapped greyboard, or a single hinged construction. Does not fold flat and is assembled by hand.
Best where perceived value carries the purchase — jewellery, watches, premium electronics, limited editions. Plan for longer lead times and higher freight volume.
Sleeve and tray
A printed sleeve slides over an inner tray. Common in confectionery and gifting because it separates the branded element from the structural one, which means one tray can serve several printed variants.
Display and counter units
Engineered so the pack becomes the shelf unit. A tear-away front opens the case into a tray with the product already faced.
Footprint has to match the retailer planogram exactly, and stacking strength must be calculated against pallet load rather than contents alone.
Trays and food containers
Open-top structures die-cut from grease-resistant board with locking corners. Speed of assembly at the counter matters as much as the print.
Choosing between styles
| Requirement | Style |
|---|---|
| Light retail product, lowest cost | Reverse tuck end |
| Weight in a folding carton | Auto-lock bottom |
| E-commerce shipping and unboxing | Roll-end tuck front |
| Bulk shipping, no presentation | Regular slotted container |
| Premium presentation | Rigid two-piece or hinged lid |
| Several printed variants, one structure | Sleeve and tray |
| Retail shelf placement | Display case with tear-away front |
| Hot or greasy food | Locking-corner tray |
Once the style is settled, the material question narrows considerably — our comparison of board grades and flute types covers what each structure should be produced on.
How structure drives cost
Style is not only an aesthetic decision. Each structure has a different board consumption, a different assembly time and a different freight profile, and those three usually matter more than the price per sheet.
Board consumption. An auto-lock bottom uses noticeably more board than a tuck end at the same finished size, because the locking base needs the extra material. On a large run that difference is real.
Assembly time. A hand-assembled tuck end costs nothing to make and costs labour to erect. On high throughput, an auto-lock that snaps open in one movement pays for its extra board in packing time within weeks.
Freight. Folding cartons ship flat. Rigid boxes ship assembled and occupy several times the volume, which is the hidden cost people miss when comparing the two on unit price alone.
Matching structure to journey
| Journey | What the structure must survive | Suitable styles |
|---|---|---|
| Handed over at a counter | Being carried by hand | Tuck end, tray, sleeve |
| Shelf then home | Facing, then a shopping bag | Tuck end, auto-lock, sleeve and tray |
| Distribution then shelf | Pallet compression, then display | Display case, regular slotted container |
| Carrier network to a doorstep | Crushing, dropping, handling | Roll-end tuck front, regular slotted container |
| Gifted in person | Being opened deliberately | Rigid two-piece, hinged lid |
The mismatch that causes most trouble is a shelf structure sent through a carrier network. A carton designed to face forward has no crush resistance and arrives looking handled.
Collapsible rigid
Worth knowing about because it sits between the two main families. A collapsible rigid box ships flat and erects into something close to a wrapped rigid structure.
It costs more than a folding carton and less than full rigid, and it feels closer to rigid than to carton. Where a premium pack has to be posted rather than handed over, it is frequently the right compromise and it is rarely offered unless asked for.
Choosing between styles
| Requirement | Style |
|---|---|
| Light retail product, lowest cost | Reverse tuck end |
| Weight in a folding carton | Auto-lock bottom |
| E-commerce shipping and unboxing | Roll-end tuck front |
| Bulk shipping, no presentation | Regular slotted container |
| Premium presentation | Rigid two-piece or hinged lid |
| Premium presentation that must post | Collapsible rigid |
| Several printed variants, one structure | Sleeve and tray |
| Retail shelf placement | Display case with tear-away front |
| Hot or greasy food | Locking-corner tray |
Once the style is settled, the material question narrows considerably — our comparison of board grades and flute types covers what each structure should be produced on.