Packaging resources
Packaging Design Checklist
A design-stage checklist covering structure, hierarchy, regulated panels, shelf legibility, print constraints and pre-flight before artwork is released.
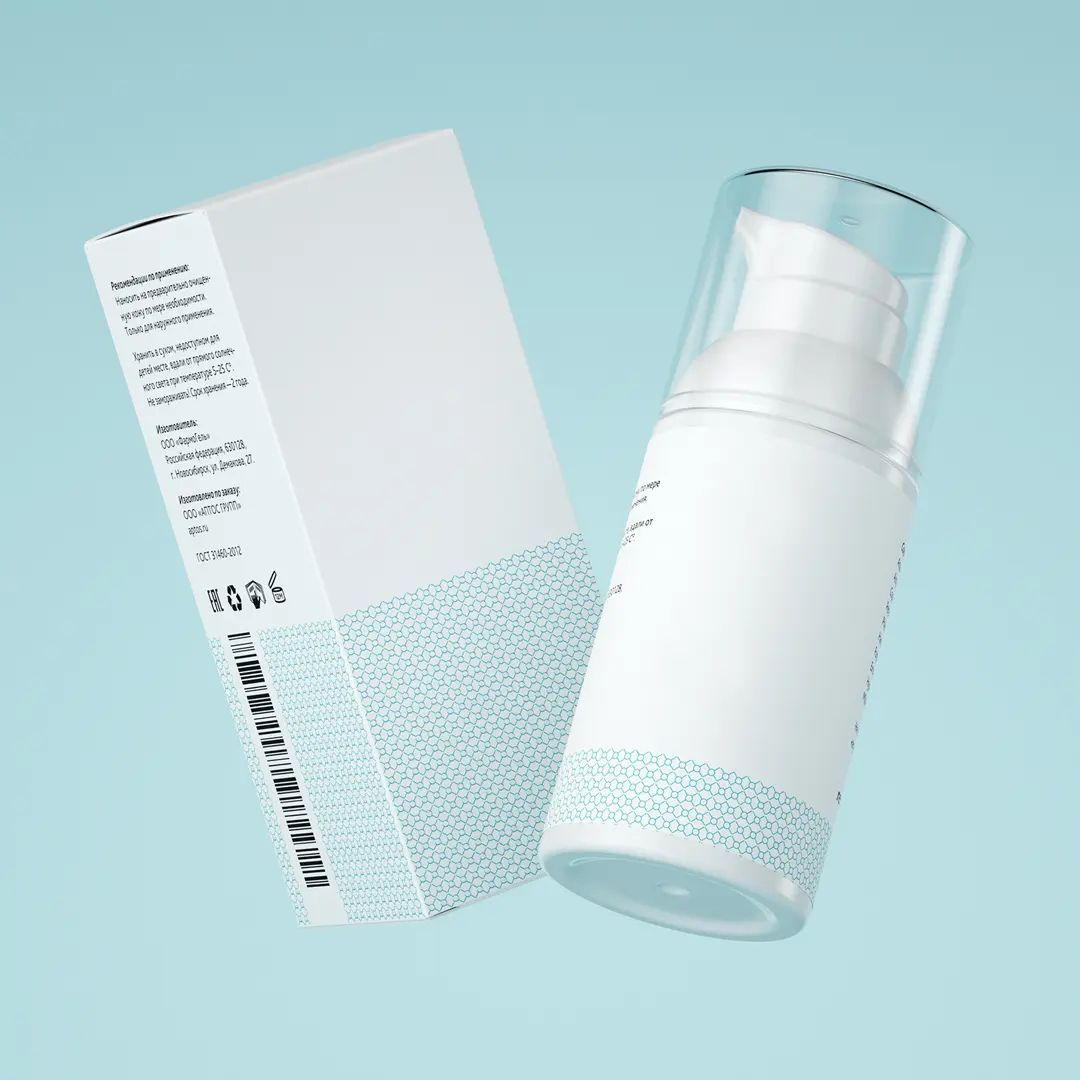
This checklist is for the design stage specifically — the decisions made between receiving a dieline and releasing artwork to production.
Before opening a design file
- Dieline received from the supplier for the confirmed size
- Panel orientation understood: which face is front, which is hidden under the glue lap
- Regulated content collected at final length, not as placeholder text
- Substrate confirmed, since kraft and uncoated stocks change colour behaviour
- Print method confirmed, since flexo and offset have different detail limits
- Finish decisions made, since spot UV and emboss need artwork designed for them
Hierarchy and legibility
- One clear primary message readable from three feet
- Brand mark positioned on the panel that faces the shopper on shelf
- Variant or flavour distinguishable at a glance from neighbouring SKUs
- Product name legible at the smallest size the pack will appear
- Secondary information genuinely secondary, not competing
Regulated panel
- Ingredient, INCI or supplement facts panel laid out at legal minimum size or larger
- Allergen declarations present and prominent where required
- Net weight, batch space and country of origin included
- State-specific warnings confirmed for every market
- Compliance sign-off obtained in writing before release
Structure interaction
- No text or barcode crossing a fold line
- Critical content held inside safety margins on every panel
- Nothing important positioned under a glue lap
- Interior print considered where the pack opens to reveal it
- Window position checked against the product inside
Print constraints
- Colour mode CMYK, spot colours named consistently
- Rich black on large solids, 100% K on small text
- Positive text above 6pt, reversed text above 8pt
- Fine detail simplified where foil or emboss is applied
- Gradients checked if printing flexo on corrugated
- Total ink coverage within press limit
Barcode
- Placed on a flat panel, not across a fold or curve
- At or above 80% of nominal size
- Dark bars on a light background with a clear quiet zone
- Scan-tested on the printed substrate, not from a screen
Pre-flight before release
- Images 300 dpi at placed size
- Fonts outlined or embedded
- Bleed on every trim edge
- Dieline layer separate and non-printing
- Unused swatches removed
- File named with product, size and version
After the proof
- Proof checked against a written specification, not memory
- Physical sample reviewed where fit or colour is critical
- Approval given by someone authorised to give it
- Approved file archived with dieline, board spec and colour targets
The technical export requirements behind several of these checks are set out in full in our packaging file requirements reference.
Designing on the dieline, not beside it
The most common structural error in packaging artwork is designing on a rectangle and transferring to the dieline afterwards. It looks equivalent and it is not.
A dieline carries information a rectangle does not: which panel is the front, where the glue lap sits, where the creases fall, which faces are hidden when the pack is assembled, and where the safety margins run. Artwork built without that information routinely places something important under a lap, across a fold or outside the safe area.
Import the dieline as a locked non-printing layer and build on top of it. Every subsequent check in this list becomes visual rather than theoretical.
What the panels are actually for
Not every face carries equal weight, and treating them equally wastes effort.
Front panel. Seen from two to three feet on a shelf. One clear message, the brand mark, and the variant. Everything else is secondary by definition.
Back panel. Read in the hand at close range. This is where regulated content lives, and where it should be laid out first at final length.
Side panels. Frequently the face a customer actually sees, because packs sit shoulder to shoulder. Narrow, and worth designing rather than filling.
Top and base. Base is generally covered or on a shelf. Top matters where products are displayed in a tray or a bin.
Interior. Free real estate on any pack that opens toward the customer, and the surface people photograph on a direct-to-consumer product.
Colour that survives production
Three practical constraints catch designs that were built without them.
Rich black on large solids and 100% K on small text. A four-colour black on 8pt type registers imperfectly and reads soft; a single-plate black stays crisp.
Total ink coverage within the press limit. Stacking four heavy channels on a dark area exceeds what the substrate can absorb, and the result is set-off and slow drying rather than a richer black.
Spot colours named consistently. A swatch called “Brand Blue” in one file and “PMS 293” in another produces two plates for one colour, and the cost of that surfaces on the invoice.
Before you release
The pre-flight list in this checklist is mechanical, and it is worth running it as a list rather than by eye. Missing bleed on one edge, an image placed at 180 dpi, or a stray unused swatch are all invisible on screen and all cost a proof cycle.
The technical export requirements behind several of these checks are set out in full in our packaging file requirements reference.