Packaging blog
How Packaging Inserts Protect and Present Products
Board, foam and moulded pulp inserts compared on protection, cost and presentation, with guidance on tolerances, cavity design and when an insert is unnecessary.
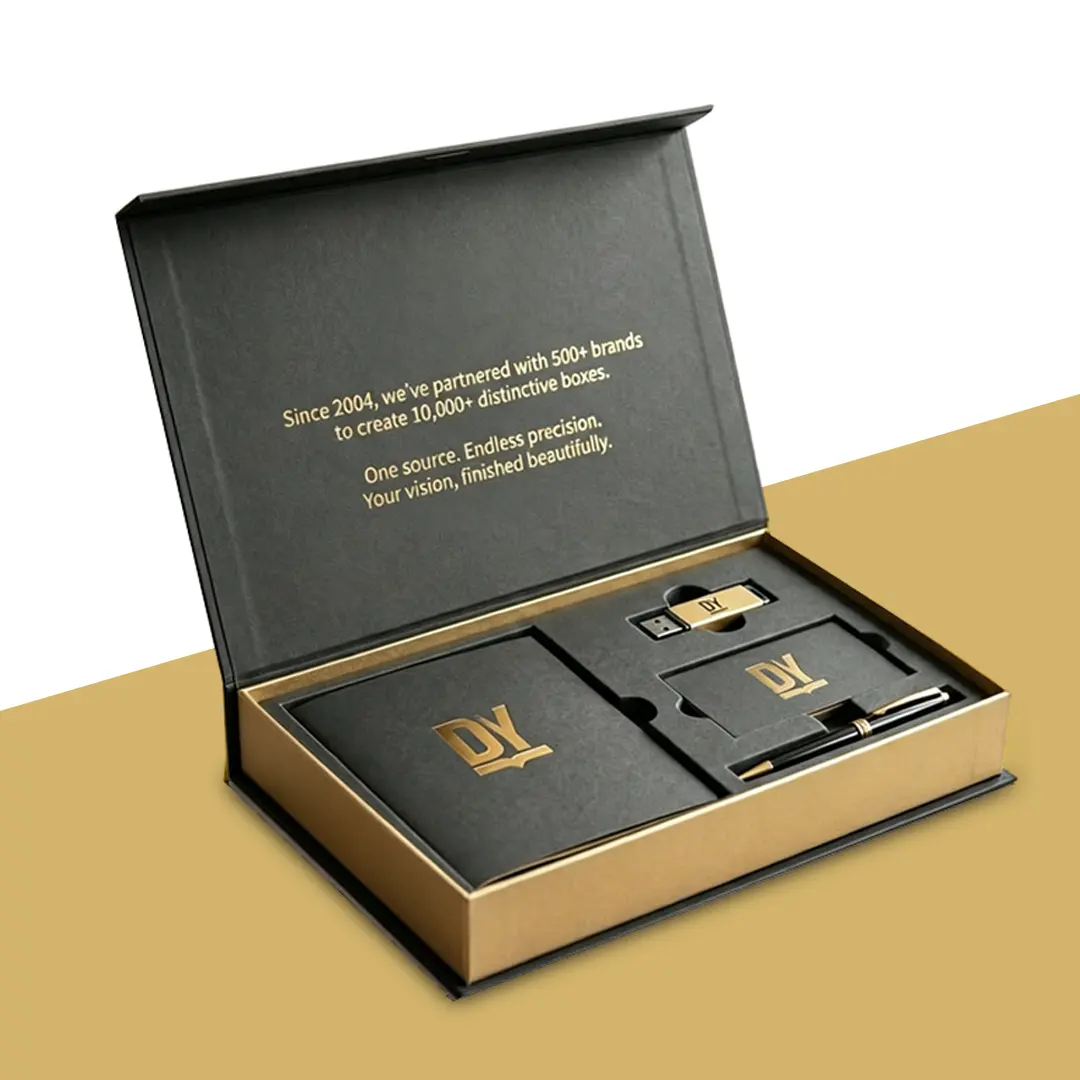
Most transit damage does not happen because the outer box failed. It happens because the product moved inside a box that survived perfectly well. An insert is the component that stops that movement, and it is routinely the cheapest reliability improvement available in a packaging specification.
It also does a second job that has nothing to do with protection. An insert decides what the customer sees at the moment of opening, and whether a multi-piece product looks organised or looks tipped into a box.
What an insert is actually doing
Three things, in order of importance.
It immobilises the product so it cannot slide, rotate or strike the walls of the outer pack. It absorbs and distributes impact energy from drops and vibration. And it positions each item so the pack presents deliberately when opened.
A pack can succeed at the first two and fail badly at the third, which is why some well-protected products still feel cheap to unbox.
Board inserts
Die-cut corrugated or chipboard is the most common insert material and handles the majority of applications.
Corrugated inserts are cut from the same E-flute or B-flute board as shipping packaging and folded or slotted into dividers, platforms and cavity trays. They are inexpensive, ship flat, and recycle with the outer box in a single stream.
Chipboard is thinner and denser, better suited to shallow trays and pads inside smaller retail packs where corrugated would be too bulky.
Board handles most products up to moderate weight. Where it struggles is with anything genuinely fragile — glass, ceramics, unprotected screens — because board resists movement well but absorbs impact poorly.
Foam inserts
Foam is what you specify when impact absorption matters more than cost.
Polyurethane foam is soft and highly absorbent, suited to delicate items. Polyethylene foam is denser and more resilient, better for heavier products and repeated handling. EVA foam is denser again with a cleaner cut edge, which is why it appears in premium presentation cases.
Foam is routed or die-cut to the product profile, which produces a snug cavity that holds the item precisely. It also looks and feels expensive, which is why it appears in electronics, instruments and high-value tool sets.
The trade-offs are cost, bulk and recyclability. Foam costs more than board, takes more space in the outer pack, and is not accepted in standard kerbside recycling.
Moulded pulp
Moulded pulp sits between the two. It is formed from recycled paper slurry pressed into a shape, so it absorbs impact better than flat board and recycles cleanly, unlike foam.
Its limitations are tolerance and finish. Moulded pulp holds looser dimensional tolerances than die-cut board or routed foam, and its surface is rough and unprintable in any detailed way. As a hidden protective layer it is excellent. As a visible presentation layer it usually is not.
Tooling for moulded pulp is also more expensive than a cutting die, so it makes sense at volume rather than for short runs.
Getting the tolerance right
This is where inserts most often go wrong, and the error is almost always in the same direction.
A cavity cut to the exact dimensions of the product will not accept the product. Manufacturing variance in both the product and the insert means an exact-fit cavity binds. Cut it too loose and the product moves, which defeats the purpose.
The workable range is generally 1 mm to 2 mm of clearance around the product for board inserts, and slightly less for foam, which compresses. Softer, more compliant products tolerate tighter cavities than rigid ones.
Include a finger cut-out. A cavity that grips a product well enough to protect it in transit is a cavity the customer cannot get the product out of, and a semicircular relief cut solves that entirely.
Designing for multi-piece products
When a pack contains several items, the insert becomes a layout decision as much as a protective one.
Decide what the customer should see first and place it in the most prominent position. Group accessories logically rather than by what fits most efficiently. Give cables and small parts their own compartment, because loose accessories rolling around the main cavity undo the impression the rest of the pack creates.
Layered inserts work well for products with a clear hierarchy — a main item on the top layer, accessories and documentation beneath. Each layer needs its own removal relief.
When you do not need one
Inserts are not free, and a pack that does not need one should not have one.
Soft goods rarely need internal structure. A folded garment is its own cushioning, and an insert in an apparel mailer adds cost, weight and material for no protective benefit.
Products that fill the outer pack completely do not need an insert either, because there is nowhere for them to move. Right-sizing the outer box is often a better answer than adding structure inside an oversized one, and it reduces dimensional weight at the same time.
Single hard-wearing items — a candle tin, a bar of soap, a hardback book — usually travel fine in a snug outer pack alone.
Getting the specification right first time
An insert is cut to the inside of the outer pack, not to the product alone, so a supplier needs both sets of dimensions. Sending only the product measurements means the insert has to be re-cut once the outer is finalised.
Send the exact dimensions of every item that needs a cavity, the weight of each, and a note on which are fragile. If the pack contains items of very different weights, say so, because a heavy item shifting next to a light one is a common damage mode.
For brands specifying protection and outer pack together, the range of packaging inserts cut to product profiles covers board, foam and multi-cavity layouts across the same production run, which keeps tolerances consistent between the insert and the box it sits in.
Testing before committing
Order a plain sample of the insert and the outer together, load it with the real product, and drop it from about a metre onto a hard floor several times on different faces.
That is not a formal test protocol, but it identifies the obvious failures immediately. If the product shifts, tighten the cavity. If the insert deforms, step up the material. If the outer creases at a corner, the load is not being distributed and the insert geometry needs work.
Doing this before a production run costs the price of one sample. Doing it after costs the run.