Packaging resources
Packaging Insert Guide
Board, foam and moulded pulp inserts compared, with cavity tolerances, multi-piece layout guidance and when an insert is not needed at all.
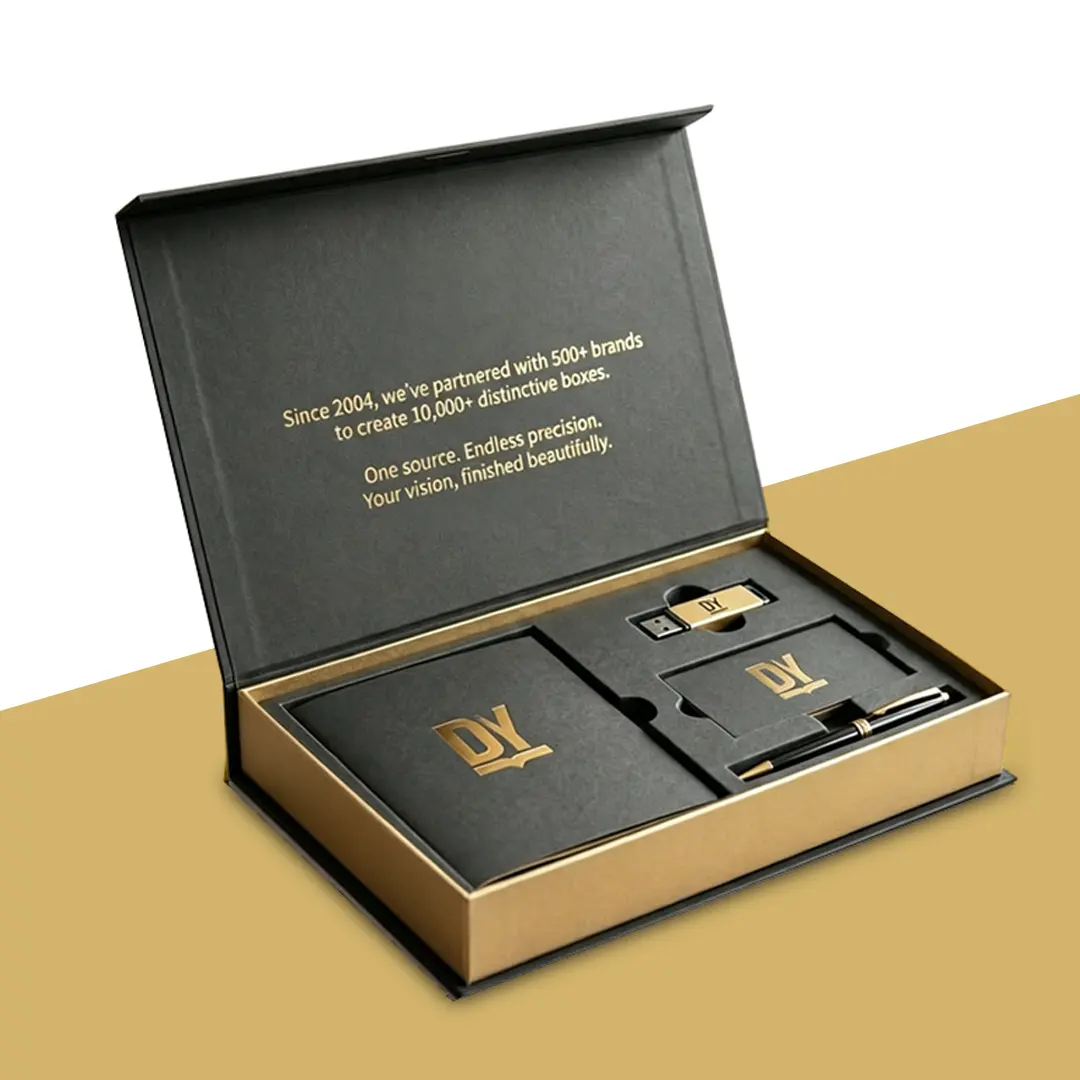
Most transit damage happens because the product moved inside a box that survived. An insert stops that movement, and it is usually the cheapest reliability improvement in a specification.
Material comparison
| Material | Protection | Cost | Presentation | Recyclable |
|---|---|---|---|---|
| Corrugated | Immobilises well, absorbs poorly | Low | Fair | Yes, with the box |
| Chipboard | Light restraint only | Low | Good in shallow trays | Yes |
| Moulded pulp | Good impact absorption | Medium | Poor surface | Yes |
| PU foam | Excellent absorption | Medium-high | Very good | No |
| EVA foam | Excellent, clean cut edge | High | Excellent | No |
Board handles most products up to moderate weight. Foam is for anything genuinely fragile — glass, ceramics, unprotected screens. Moulded pulp sits between the two but cannot be a visible presentation layer.
Cavity tolerance
A cavity cut to exact product dimensions will not accept the product. Manufacturing variance in both means an exact fit binds.
Allow 1 mm to 2 mm clearance around the product for board inserts, slightly less for foam, which compresses. Softer products tolerate tighter cavities than rigid ones.
Always include a finger relief cut. A cavity that grips well enough to protect in transit is one the customer cannot get the product out of.
Multi-piece layout
Decide what the customer should see first and give it the most prominent position. Group accessories logically rather than by what packs most efficiently. Give cables and small parts their own compartment.
Layered inserts suit products with a clear hierarchy — main item on top, accessories beneath. Each layer needs its own removal relief.
When you do not need one
Soft goods rarely need internal structure; a folded garment cushions itself. Products that fill the outer pack completely have nowhere to move. Single hard-wearing items usually travel fine in a snug outer alone.
Right-sizing the outer box is frequently a better answer than adding structure inside an oversized one, and it reduces dimensional weight at the same time.
Specifying correctly
An insert is cut to the inside of the outer pack, not to the product alone, so both sets of dimensions are needed. Send the exact measurements and weight of every item requiring a cavity, and flag which are fragile.
Where items of very different weights sit together, say so — a heavy item shifting beside a light one is a common damage mode.
Testing
Order a plain sample of insert and outer together, load it with the real product and drop it from about a metre onto a hard floor on several faces.
If the product shifts, tighten the cavity. If the insert deforms, step up the material. If the outer creases at a corner, load is not being distributed and the geometry needs work. Our guide to measuring products and allowing clearance covers the dimension side of the same problem.
Transit fit and presentation fit are different jobs
An insert that grips a product firmly for transit is usually invisible and slightly tight. An insert that presents a product on opening seats it loosely and is part of what the recipient sees. Asking one part to do both tends to compromise one of them.
Decide which matters more before anything is cut. Where both genuinely matter — premium electronics, fragrance, gift sets — the answer is normally a presentation layer inside a protective outer rather than one clever component trying to do everything.
Reading a damage report
Damage patterns point directly at the fix, and misreading them is what produces expensive changes that do not work.
| What arrives | What it means | What to change |
|---|---|---|
| Box crushed, contents intact | Board too light for the stack | Heavier flute, or better palletisation |
| Box intact, contents damaged | Product moved inside | Fitted insert |
| Corner crushed, contents fine | Impact on a drop | Corner protection or a deeper insert |
| Contents scuffed, nothing broken | Product rubbing the cavity | Softer cavity face or a liner |
| Damage only on one route | Carrier handling, not the pack | Specify for the harshest network |
The distinction that matters most is the first two rows. They look similar on a summary report and need opposite responses.
Cost behaviour
Inserts carry a tooling cost — a cutting die for board and foam, a mould for pulp — plus a per-unit cost. Board tooling is inexpensive and pulp tooling is not, which is why moulded pulp only makes sense at volume even where it is technically the better answer.
That gives a rough hierarchy for short runs: board first, foam second, pulp only when the quantity justifies the mould.
Testing
Order a plain sample of insert and outer together, load it with the real product and drop it from about a metre onto a hard floor on several faces.
If the product shifts, tighten the cavity. If the insert deforms, step up the material. If the outer creases at a corner, load is not being distributed and the geometry needs work. Our guide to measuring products and allowing clearance covers the dimension side of the same problem.